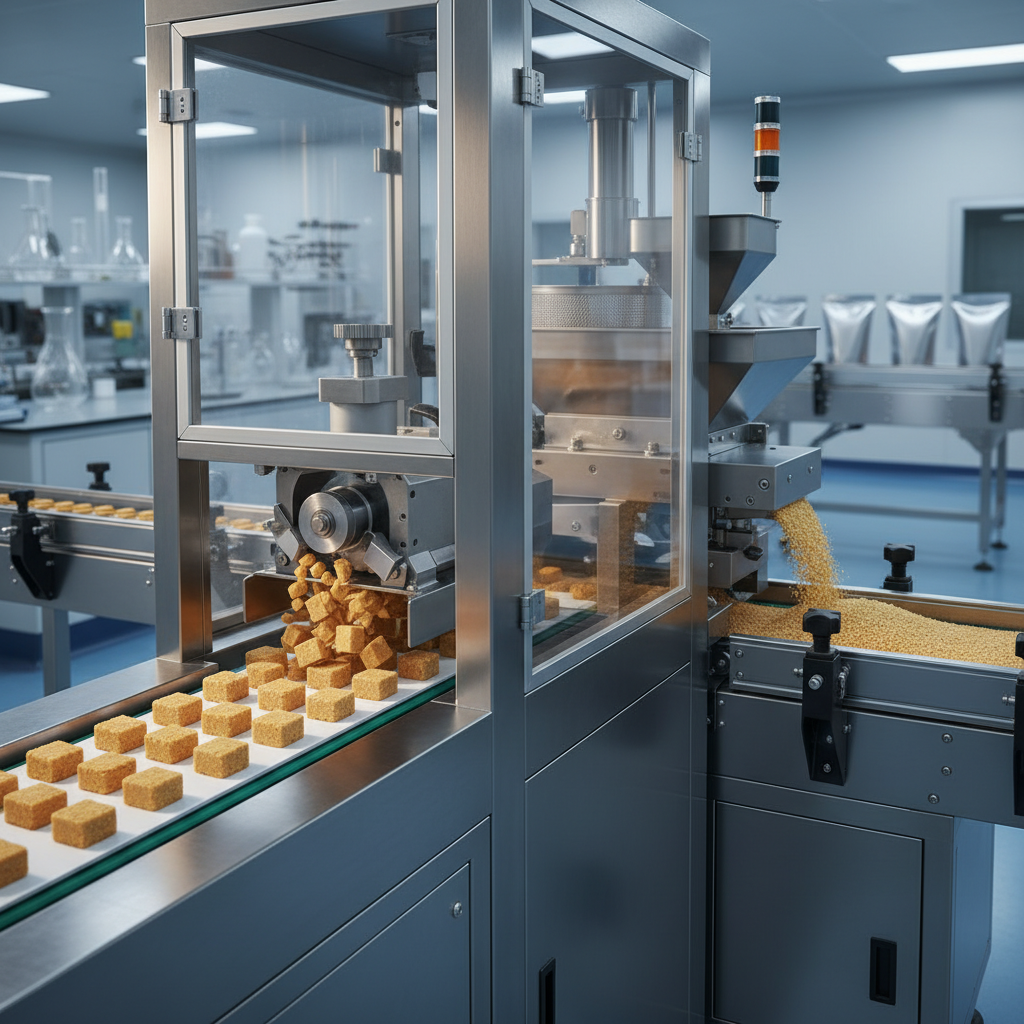
The global market for high-intensity sweeteners has seen a significant shift toward low-calorie alternatives that maintain a superior taste profile. For businesses looking to optimize their supply chain, finding a reliable partner to buy feed additive distributor services is essential to ensuring that raw materials like Aspartame meet stringent purity and safety standards.
Aspartame, a low-calorie sweetener composed of L-Aspartic Acid and L-Phenylalanine, has become a cornerstone in the production of sugar-free goods. As industries scale, the demand for a consistent, high-capacity supply—such as the 500mt/month productivity offered by top-tier manufacturers—highlights the importance of strategic sourcing and distribution.
Whether you are operating in the beverage, pharmaceutical, or confectionery sector, the ability to buy feed additive distributor quality products ensures your final formulations remain stable, cost-effective, and compliant with international certifications like ISO 9001:2008 and FDA.
Understanding Aspartame Purity and Sourcing
Aspartame is a highly efficient, low-calorie sweetener that is approximately two hundred times sweeter than sucrose. Because it consists of two common amino acids, it integrates seamlessly into various food and pharmaceutical matrices. When companies decide to buy feed additive distributor materials, they prioritize purity levels, typically requiring an assay of 98%-102% on a dry basis to ensure consistent sweetness and flavor stability.
The versatility of Aspartame is further enhanced by its available forms, ranging from powder to granular types from 20 mesh to 350 mesh. This flexibility allows manufacturers to choose the exact particle size needed for their specific production process, whether it be for instant powdered mixes or high-clarity liquid syrups.
Global Market Dynamics of Sweetener Distribution
The global movement toward sugar reduction has placed immense pressure on the supply chains of intensive sweeteners. As consumers demand healthier alternatives without sacrificing taste, the role of a distributor becomes critical in bridging the gap between China-origin factories and international markets. Efficient distribution ensures that high-volume productivity, such as 500mt per month, is allocated effectively across different regions.
Challenges in the global market often stem from volatile shipping costs and varying regional regulations. By partnering with a distributor who manages ocean, land, and air transportation, companies can mitigate the risks of stockouts and price fluctuations. This systemic approach to sourcing allows for a more stable production cycle in the beverage and confectionery industries.
Furthermore, the integration of Halal and ISO certifications into the distribution process allows for wider market penetration. When buyers look to buy feed additive distributor options, they are not just purchasing a chemical compound, but a certified guarantee of safety and quality that meets the standards of the FDA and other global health authorities.
Technical Specifications and Quality Control
Quality control is the bedrock of sweetener manufacturing. For Aspartame, critical parameters include the specific rotation (+14.5º to +16.5º) and the strict limitation of Diketopiperazine (DKP) to ≤ 1.5%. Maintaining these levels is essential for those who buy feed additive distributor products to avoid off-flavors or instability in the final product.
The chemical purity is further validated by monitoring the Loss on Drying (≤ 4.5%) and Residue on Ignition (≤ 0.2%). These metrics ensure that the material is free from excessive moisture and inorganic impurities, which is a primary concern for pharmaceutical companies that buy feed additive distributor grade sweeteners for tablets and syrups.
Safety thresholds for heavy metals are non-negotiable, with Lead kept ≤ 10 mg/kg and Arsenic ≤ 3 mg/kg. Additionally, microbial control—limiting Total Bacteria Count to ≤ 250cfu/g—ensures that the Aspartame is safe for human consumption across thousands of product lines worldwide.
Industrial Application Efficiency Analysis
Aspartame's application spans a diverse array of industries, from carbonated soft drinks to effervescent pharmaceutical tablets. Its high potency means that very small quantities are required to achieve the desired sweetness, significantly reducing raw material costs and shipping weights. This efficiency is why many procurement managers seek to buy feed additive distributor channels that can provide bulk quantities of 25kg drums.
In the confectionery sector, Aspartame is used in chewing gums and jellies to provide a clean sweetness that does not crystallize. In the dairy industry, it enhances the flavor of low-calorie yogurts and frozen desserts, maintaining a creamy texture without the bulk of traditional sugars.
Performance Metrics for Sourcing via buy feed additive distributor
Logistics and Supply Chain Scalability
Scalability is achieved through a combination of high production capacity and diversified transportation methods. With a supply ability of 500mt per month, the manufacturing process is designed to handle sudden spikes in demand from global beverage brands. This ensures that when clients buy feed additive distributor shipments, they receive their orders without production delays.
The use of standard 25kg paper drums provides a balance between protection and ease of handling. By leveraging the Port of Shanghai, products are efficiently routed via ocean freight for bulk orders, while air freight is utilized for urgent, smaller shipments, ensuring that the supply chain remains agile and responsive to market needs.
Regulatory Compliance and Safety Standards
Compliance with international standards is not optional in the food additive industry. Aspartame is approved for human consumption in most countries, but maintaining this status requires rigorous adherence to FDA and ISO 9001:2008 guidelines. This regulatory rigor is a key selling point for those who buy feed additive distributor products for export into highly regulated markets like the EU or North America.
The inclusion of Halal certification further expands the usability of the product, allowing it to be used in food production for diverse cultural and religious demographics. This comprehensive certification approach reduces the burden of proof for the end-manufacturer, who can rely on the distributor's documentation.
Safety is further reinforced through the monitoring of L-phenylalanine levels (≤ 0.5%) and pH levels (4.5-6.0). These specific parameters ensure that the product is chemically stable and safe for the intended population, provided that standard labeling requirements for phenylketonuria are followed.
Strategic Comparison of Distribution Models
Choosing the right sourcing model is critical for long-term profitability. Direct factory sourcing offers the lowest price point and the highest level of quality control, making it ideal for high-volume users. However, regional distributors offer the advantage of lower lead times and localized support, which is often more attractive for mid-sized enterprises looking to buy feed additive distributor options.
A hybrid model, combining bulk shipments from China with local warehousing, often provides the best balance of cost and agility. This strategy allows companies to lock in prices based on 500mt/month productivity while maintaining a safety stock for immediate production needs.
Ultimately, the value of a distribution partner lies in their ability to provide consistent assay results (98%-102%) and reliable logistics. Whether through ocean or air freight, the stability of the supply chain directly impacts the manufacturer's ability to maintain their own delivery schedules and product quality.
Comparison Analysis of Aspartame Sourcing Channels
| Sourcing Method |
Lead Time |
Cost Efficiency |
Quality Assurance |
| Direct Factory |
Long (Ocean) |
High (Lowest Cost) |
Maximum Control |
| Regional Distributor |
Short |
Moderate |
Standardized |
| Global Trading Hub |
Medium |
Moderate |
Variable |
| Air Freight Agent |
Very Short |
Low (Expensive) |
High |
| Bulk Procurement Co. |
Medium |
High |
Consistent |
| Specialty Broker |
Variable |
Low |
Niche Verified |
FAQS
A high-quality Aspartame supplier typically provides an assay of 98% to 102% on a dry basis. This range ensures the sweetener performs consistently in low-calorie beverages and pharmaceutical applications without altering the intended taste profile.
You should look for ISO 9001:2008, FDA approval, and Halal certification. These ensure that the manufacturing process meets global quality management standards and is suitable for a wide range of international dietary requirements.
Yes, Aspartame is widely used in pharmaceuticals for sugar-free syrups, chewable tablets, and effervescent tablets. Its high intensity allows for small dosing, which is ideal for maintaining the physical integrity of medical tablets.
The industry standard for bulk Aspartame is 25kg paper drums. This packaging protects the powder or granular material from external contaminants while being efficient for palletization and transportation via ocean or land freight.
Mesh size (ranging from 20 to 350 mesh) determines the dissolution rate. Finer powders (higher mesh) dissolve more quickly in liquids, making them ideal for instant beverage mixes, while granular types may be preferred for certain confectionery uses.
Top-tier factories typically offer a productivity and supply ability of approximately 500mt per month, ensuring they can support large-scale global beverage and food production needs without interruption.
Conclusion
In conclusion, the strategic sourcing of Aspartame requires a careful balance of purity specifications, regulatory compliance, and logistics efficiency. By prioritizing distributors who can guarantee an assay of 98%-102% and provide comprehensive certifications like ISO and FDA, manufacturers can ensure their low-calorie products remain competitive and safe. The ability to scale production through a 500mt/month capacity ensures that global demand for sugar-free alternatives is met with consistency.
Looking forward, the integration of more agile supply chains and a commitment to strict quality control will define the leaders in the sweetener industry. Companies are encouraged to evaluate their distribution models to optimize lead times and costs. For those seeking a reliable partner to enhance their product lines, we invite you to visit our website: www.standard-seasoning.com.