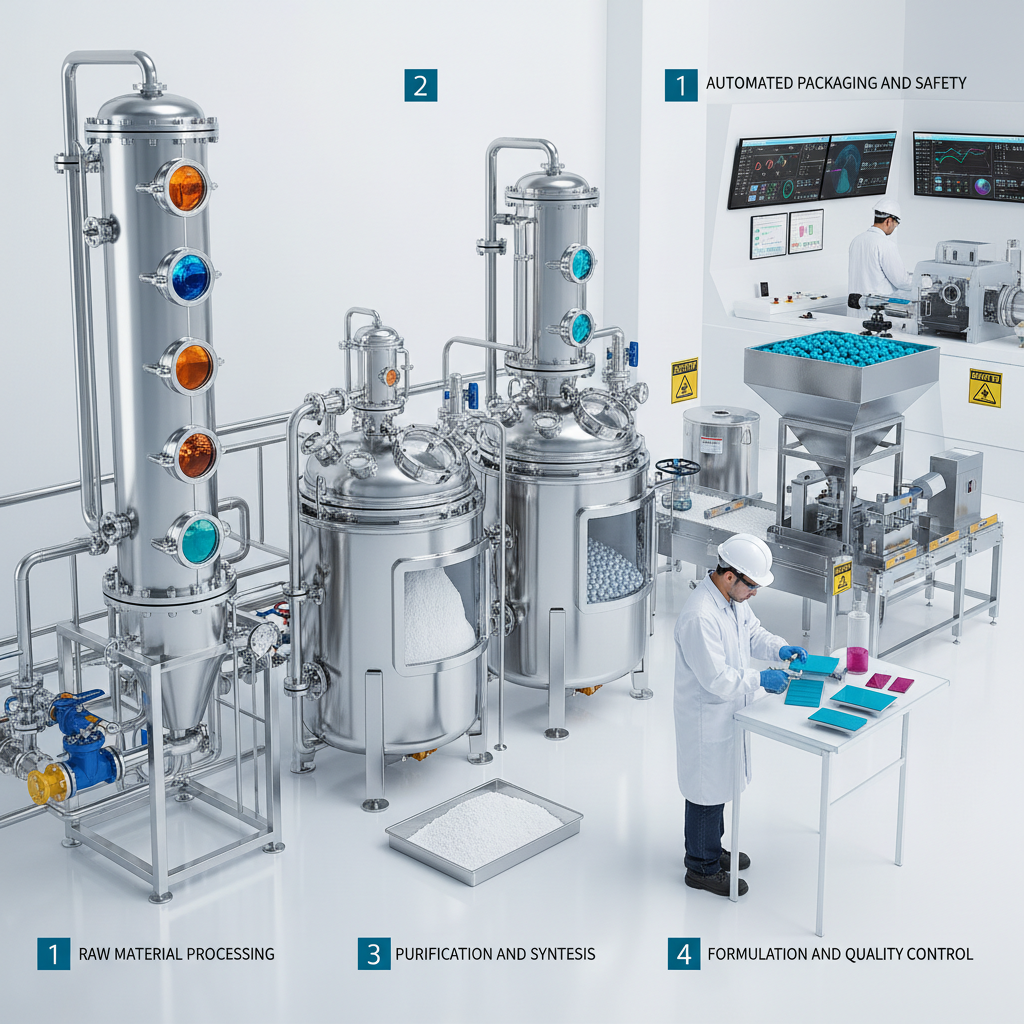
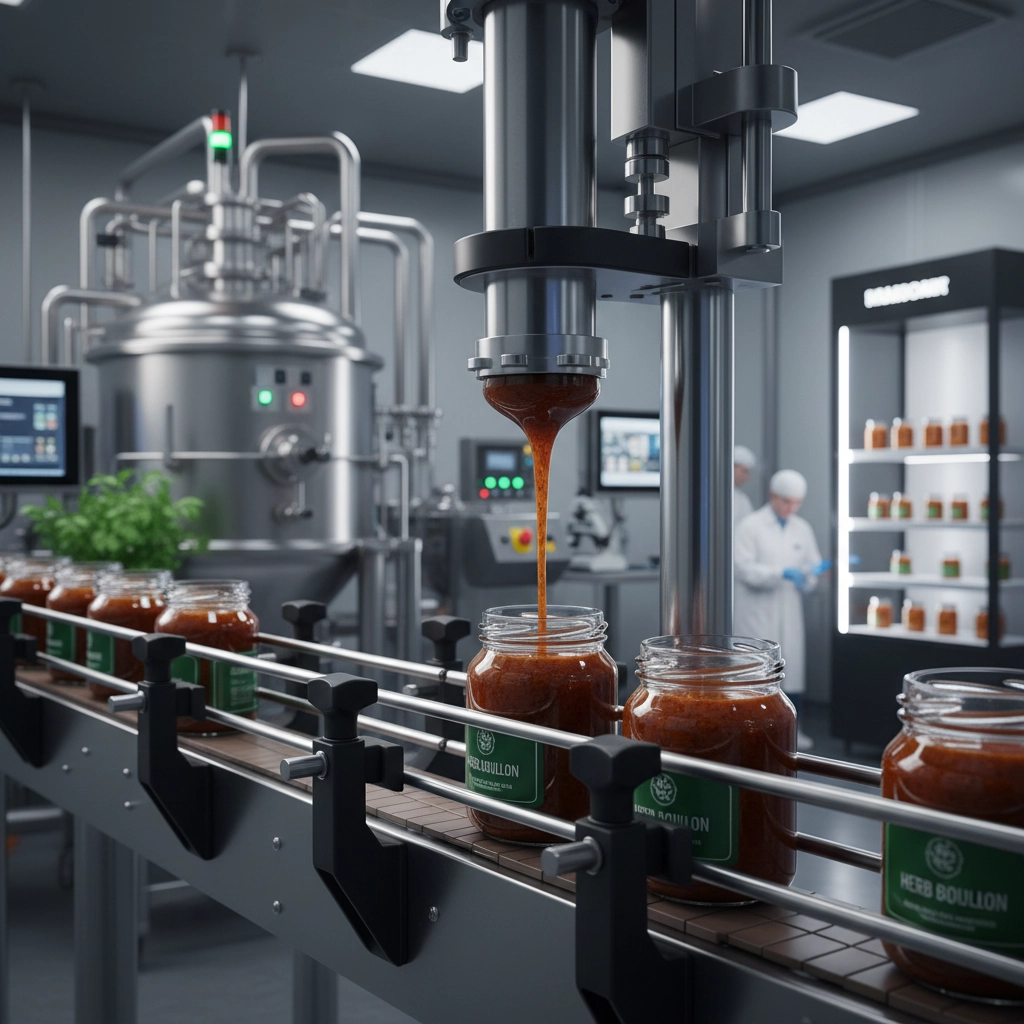
The global demand for high-quality seasoning and nutritional additives has led to a sophisticated evolution in how flavor enhancers are produced and distributed. In the broader context of additive manufacturing, whether focusing on human consumption or industrial applications, the precision of the production process ensures that taste, stability, and nutritional value are maintained across various international markets.
Maintaining consistency in mass production is a primary challenge for any additive facility, requiring strict adherence to international safety standards. From the selection of raw materials like palm oil and salt to the final packaging in aluminum foil, every step is designed to maximize shelf life and flavor potency, ensuring that consumers receive a product that tastes fresh and authentic.
While some industry players may search for an animal feed enzymes factory, it is crucial to distinguish between agricultural enzymes and high-grade human food seasonings. Our focus remains on providing premium bouillon cubes—including beef, chicken, and shrimp flavors—that meet rigorous HALAL, ISO, and FDA certifications for the global food additive market.
Quality Standards in Additive Production
Quality assurance is the cornerstone of any professional manufacturing plant. For bouillon cubes, this means ensuring that every single piece—whether it is the 4g or 10g specification—contains the exact ratio of salt, palm oil, and flavor enhancers to provide a consistent taste profile. This precision prevents flavor variance and ensures that a cup of beef soup tastes the same regardless of the batch.
Moreover, the integration of advanced workmanship allows for a production capacity of 500mt per month. By optimizing the mixing and pressing stages, the factory ensures that the cubes are durable enough for transport yet dissolve quickly in hot water, providing a seamless user experience for wholesalers and end consumers alike.
Core Components of Seasoning Cubes
The efficacy of a seasoning cube relies on its primary ingredients, which must be sourced for purity and stability. Salt acts as the primary preservative and flavor base, while palm oil and vegetable fats provide the necessary texture and mouthfeel. Flavor enhancers and MSG are carefully balanced to create the deep, savory "umami" profile found in chicken, beef, and seafood varieties.
Beyond the taste, the physical structure of the cube is essential. The compression process ensures that the ingredients remain compact during storage but are readily available upon heating. This balance of chemistry and physics allows the product to maintain a shelf life of 24 months when kept in a cool, dry place away from direct sunlight.
While industrial buyers might compare these processes to those in an animal feed enzymes factory, the food-grade requirements are significantly more stringent. Every ingredient must be food-safe and certified, ensuring that the resulting bouillon cube is not only tasty but also safe for global consumption across different dietary laws.
Global Market Applications and Distribution
Our products are strategically distributed to major markets including Africa, the Middle East, and mainland China. The versatility of the bouillon cube—available in flavors like onion, tomato, fish, and vegetable—makes it a staple in diverse culinary traditions, providing an affordable way to enhance the nutritional and taste profile of home-cooked meals.
Logistics play a critical role in maintaining product integrity. Shipping via ocean, land, or air from the Port of Qingdao ensures that the animal feed enzymes factory standards of precision are mirrored in our food additive logistics, utilizing five-layer corrugated paper cartons to prevent crushing during transit.
The ability to offer customized packing is a key competitive advantage. Whether a client requires side packing or envelope packing for 10g cubes, our flexibility allows us to meet the specific branding and regulatory needs of different regions, ensuring a high success rate for wholesale distributors.
Production Scalability and Efficiency
Scalability in the additive industry requires a harmony between raw material procurement and machine output. With a supply ability of 500mt per month, the facility is equipped to handle large-scale wholesale orders starting from a MOQ of 1000 cartons. This volume is achieved through automated pressing and wrapping lines that minimize human error and contamination.
The efficiency of the production line is measured not just by volume, but by the consistency of the 4g and 10g specifications. Each specification is optimized for specific market preferences, ensuring that the packaging—from the three-layer aluminum foil to the outer carton—is perfectly fitted to the product size to reduce waste.
Efficiency Metrics for Additive Production Lines
Packaging Innovation for Long-Term Stability
Packaging is more than just a container; it is a protective barrier that preserves the volatile flavor compounds of the bouillon cubes. The use of three-layer aluminum foil for individual pieces prevents moisture ingress and oxidation, which is critical for maintaining the 24-month shelf life.
To ensure these delicate foils survive the journey from China to Africa or the Middle East, the outer packaging utilizes high-strength five-layer corrugated paper. This multi-tiered approach to protection guarantees that the product arrives in pristine condition, regardless of the transportation method used.
Certification and Compliance Frameworks
In the food additive industry, certifications are the primary indicators of trust and safety. Our facility operates under a comprehensive compliance framework including ISO9000 and ISO22000, which govern quality management and food safety systems. These standards ensure that every batch of bouillon is produced in a hygienic environment.
Furthermore, HALAL and HACCP certifications allow our products to enter diverse cultural and religious markets with confidence. By adhering to these strict guidelines, we eliminate the risk of cross-contamination and ensure that the ingredients used are permissible and safe for all consumers.
FDA approval further expands our reach, allowing us to meet the stringent safety requirements of the North American market. This commitment to certification mirrors the rigorous quality checks found in any top-tier animal feed enzymes factory, ensuring a scientific approach to additive safety.
Future Trends in Food Additive Manufacturing
The future of bouillon production is moving toward cleaner labels and the reduction of synthetic additives. We are exploring ways to enhance the natural flavor profile of our beef and chicken cubes while maintaining the same high level of productivity and cost-efficiency that our wholesale partners expect.
Digital transformation in the factory setting, including AI-driven quality control and automated inventory management, is helping us reduce waste and improve delivery times. By optimizing the supply chain, we can reduce the shipping window to 7-15 days upon deposit, enhancing the agility of our global partners.
Sustainability is also becoming a priority, with a focus on more eco-friendly packaging materials that do not compromise the protective qualities of aluminum foil. As the industry evolves, the goal is to create a production cycle that is as sustainable as it is efficient.
Analysis of Product Specifications and Logistics Capacity
| Specification Type |
Packaging Detail |
Container Load (20ft) |
Market Suitability |
| 10g/pc (60pcs box) |
24 boxes/carton |
1850 Cartons |
Premium Retail |
| 10g/pc (48pcs box) |
30 boxes/carton |
1850 Cartons |
Standard Wholesale |
| 4g/pc (25pcs sachet) |
80 sachets/carton |
2300 Cartons |
Economy Market |
| 4g/pc (50pcs sachet) |
40 sachets/carton |
2300 Cartons |
Mid-Tier Retail |
| 4g/pc (100pcs bag) |
20 bags/carton |
2300 Cartons |
Bulk Institutional |
| Customized Packing |
Tailored to Client |
Variable |
Private Label |
FAQS
We offer a wide range of professional flavors including chicken, beef, shrimp (crayfish), onion, fish, vegetable, and tomato. Each flavor is crafted to provide an authentic taste that allows users to create fresh-tasting soups and seasoned dishes with just a single cube.
Our products are fully compliant with international safety and quality standards, holding certifications such as HALAL, QS, ISO9000, ISO22000, HACCP, and FDA. This ensures our seasoning cubes meet the strict import requirements of the Middle East, Africa, and other global regions.
Our bouillon cubes have a shelf life of 24 months. To maintain optimal quality and flavor potency, they should be stored in a cool, dry place and kept away from direct sunlight. The three-layer aluminum foil packaging helps prevent moisture and air from degrading the product.
Yes, customized packing is available to meet specific market needs. We provide various options including side packing and envelope packing for our 10g cubes, and multiple sachet or bag configurations for 4g cubes, ensuring your brand can enter the market with a tailored presentation.
The Minimum Order Quantity is 1000 cartons. Once the deposit is received, the delivery time is typically between 7 to 15 days. We ship via ocean, land, or air, primarily through the Port of Qingdao to ensure efficient global distribution.
Our factory has a high productivity rate of 500mt per month. With streamlined automated processes and a robust supply chain for ingredients like palm oil and salt, we can reliably fulfill large-scale orders while maintaining strict quality control across all batches.
Conclusion
In summary, the production of high-quality bouillon cubes requires a precise intersection of food science, strict quality certification, and robust logistics. From the meticulous selection of ingredients to the use of multi-layered aluminum and corrugated packaging, every detail is engineered to provide a consistent, delicious, and long-lasting product for the global market. By maintaining certifications such as ISO, HALAL, and FDA, we ensure that our additives meet the highest safety standards required by wholesalers and consumers worldwide.
Looking forward, the industry will continue to embrace automation and sustainable packaging to meet the evolving demands of the global food supply chain. For businesses seeking a reliable partner in food additives, prioritizing a manufacturer with proven productivity and a commitment to international standards is the key to long-term success. Visit our website for more information: www.standard-seasoning.com