Monosodium glutamate vetsin is one of the most widely utilized flavor enhancers in the global food industry, renowned for its ability to impart the savory "umami" taste. As a salt of glutamic acid, it bridges the gap between nutritional requirements and culinary satisfaction, allowing food manufacturers to enhance the palatability of a vast array of products. Understanding its role is essential for anyone involved in food science or large-scale food production.
In the competitive landscape of food additive manufacturing, the production of high-purity monosodium glutamate vetsin requires rigorous control over crystallization and precipitation processes. The goal is to achieve a product that is not only chemically pure—typically with a content of 99%—but also physically appealing, featuring transparent, bright, and uniform crystals. This technical precision ensures that the additive integrates seamlessly into different food matrices without altering the texture.
From industrial applications in salted foods to its use as a laboratory reagent, the versatility of monosodium glutamate vetsin makes it an indispensable tool for enhancing taste profiles. Whether it is used at concentrations of 0.2-0.9% in food or combined with sugar to mask the bitterness of pharmaceutical drugs, its impact on the sensory experience of consumption is profound and globally recognized.
The Technical Process of Monosodium Glutamate Vetsin Crystallization
The production of monosodium glutamate vetsin begins with a sophisticated crystallization and precipitation sequence. This process is meticulously divided into stages: concentration, seed crystallization, growth, and finally, pot release. To ensure the final crystal is uniform and bright, the neutralizer used must have minimal impurities and a light transmittance exceeding 90%, which prevents discoloration of the final product.
Crystallization is triggered when the concentrated solution reaches 30~30.5 Be at 70 ℃. At this stage, crystal seeds are introduced. A critical phenomenon known as "pseudocrystals" (small new nuclei) often appears; to manage this, producers employ a "whole crystal" technique, where warm water is added to dissolve these small nuclei without melting the primary crystal seeds, ensuring a consistent grain size.
Quality Specifications and Purity Standards
The commercial value of monosodium glutamate vetsin is directly tied to its chemical purity and physical appearance. A high-standard product typically maintains a content of 99%, ensuring that the flavor enhancement is potent and consistent. Key purity indicators include a transmittance of 98%, which reflects the clarity and brightness of the crystals, and strictly controlled levels of contaminants such as Chloride (0.1%) and Sulfate (0.05%).
Beyond these parameters, heavy metal content and iron levels are monitored to meet food safety regulations. For instance, iron is kept at 5ppm and heavy metals at 10ppm. The pH level is maintained between 6.7 and 7.5, ensuring the additive remains stable during storage and when blended with other food ingredients, preventing adverse chemical reactions.
These specifications are not merely numbers but are the result of precise manufacturing. By controlling the mother liquor after centrifugation—which still contains significant amounts of the product—manufacturers can recycle the material into the next neutralization batch, maximizing yield while maintaining the strict quality thresholds required for global export.
The Role of Supersaturation in Crystal Growth
Maintaining a low supersaturated state is the secret to producing high-quality monosodium glutamate vetsin. During the growth phase, diluted decoloring solutions are added based on the concentration of the feed solution. This prevents the sudden generation of new crystal nuclei and encourages the continuous growth of existing crystals, leading to the desired uniform particle size.
The process of promoting grain growth through strategic feeding is a delicate balance. If the concentration fluctuates too wildly, the crystals may become irregular. Therefore, the feed solution is carefully managed to ensure that the growth rate of the grains outweighs the formation of new nuclei, resulting in the characteristic transparency of monosodium glutamate vetsin.
Once the grains reach the required size, the process transitions to discharge. Before the pot is released, warm water at the same temperature is added to reduce the concentration to 29-39.5Be. This preparation step ensures that the centrifuge process is efficient and that the separated crystals maintain their structural integrity.
Industrial Applications and Dosage Efficiency
In the food manufacturing sector, monosodium glutamate vetsin is primarily used as a flavor enhancer. Its efficiency is remarkable, as it is typically used in concentrations of only 0.2% to 0.9% in normally salted foods. This low dosage allows manufacturers to achieve a deep, savory profile without overwhelming the natural flavors of the ingredients or excessively increasing the cost of production.
Beyond basic seasoning, the application of this additive extends to complex food matrices where it works synergistically with other ingredients to improve palatability. Its ability to stimulate taste receptors makes it a global standard in the production of snacks, soups, and processed meats, providing a consistent taste experience regardless of the regional variations in raw materials.
Application Efficiency of Monosodium Glutamate Vetsin
Advanced Drying and Packaging Methods
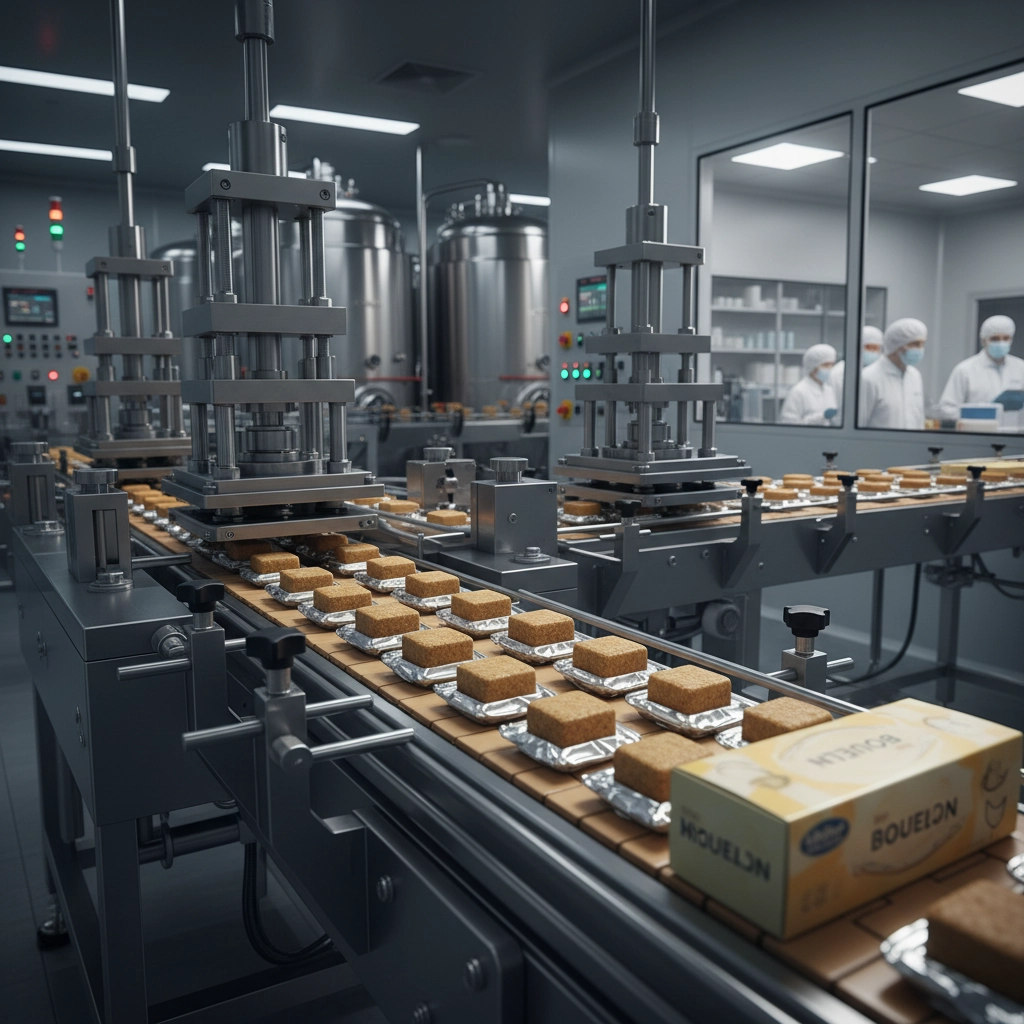
After the centrifugation process, the separated crystals of monosodium glutamate vetsin must be dried to prevent clumping and ensure long-term stability. Modern facilities employ a variety of drying technologies depending on the required scale and energy efficiency, including box drying rooms, vacuum box drying, airflow drying, conveyor belt drying, and vibrating bed drying.
To maintain the marketability of the product, uniformity in particle size is non-negotiable. Following the drying phase, the crystals are screened using vibrating screens. This critical step removes oversized or undersized particles, ensuring that the final packaged product consists of uniform, high-quality grains that meet the expectations of industrial buyers.
Pharmaceutical and Laboratory Utility
While predominantly known as a food additive, monosodium glutamate vetsin has significant utility in the pharmaceutical industry. One of its most clever applications is its use in combination with sugar to improve the palatability of bitter drugs. By masking unpleasant tastes, it increases patient compliance, particularly in pediatric medicine where taste is a major barrier to treatment.
In a scientific context, the high purity of the crystallized product allows it to serve as a reliable laboratory reagent. Because the manufacturing process ensures a content of 99% and strict control over heavy metals, it provides a consistent baseline for biochemical research and analysis.
The versatility of monosodium glutamate vetsin thus extends from the kitchen to the pharmacy and the lab. This multi-sector utility underscores the importance of maintaining rigorous production standards, as a reagent requires a different level of scrutiny than a bulk food additive.
Comparative Analysis of Production Parameters
Optimizing the production of monosodium glutamate vetsin requires a deep understanding of how different variables affect the final yield and quality. For instance, the balance between temperature and concentration during the "whole crystal" phase determines whether the product will be a fine powder or the preferred bright, transparent crystal.
Another critical factor is the management of the mother liquor. By incorporating the residue from centrifugation back into the neutralization solution, manufacturers can significantly reduce waste. This closed-loop approach not only lowers the cost of production but also reduces the environmental impact of the manufacturing plant.
Ultimately, the combination of precise chemical specifications and mechanical processing defines the grade of the product. Whether intended for food, pharma, or research, the focus remains on purity, transmittance, and particle uniformity.
Analysis of Monosodium Glutamate Vetsin Production Quality Metrics
| Metric Category |
Standard Specification |
Impact on Quality |
Control Method |
| Purity (Content) |
99% |
Flavor Potency |
Crystallization Control |
| Transmittance |
98% |
Visual Clarity |
Neutralizer Purity |
| Iron Level |
5ppm |
Color Stability |
Raw Material Screening |
| Heavy Metals |
10ppm |
Food Safety |
Strict Filtration |
| PH Range |
6.7 - 7.5 |
Chemical Stability |
Neutralization Stage |
| Particle Size |
Uniform |
Solubility Rate |
Vibrating Screening |
FAQS
For most normally salted foods, the recommended concentration is between 0.2% and 0.9%. This range is sufficient to enhance the savory umami profile without altering the original characteristics of the food. Using it within this range ensures optimal palatability and cost-efficiency for the manufacturer.
Clarity is ensured by using a neutralizer with very low impurities and a light transmittance of more than 90%. Additionally, maintaining a low supersaturated state during the growth phase prevents the formation of cloudy pseudocrystals, resulting in a final product with a transmittance of 98%.
Yes, it is frequently used in the pharmaceutical industry, particularly when combined with sugar. This combination helps to improve the palatability of bitter medicines, making them easier for patients to consume, especially in pediatric formulations.
Common drying methods include box drying rooms, vacuum box drying, airflow drying, conveyor belt drying, and vibrating bed drying. The choice depends on the desired throughput and the specific crystal size of the product being processed.
The "whole crystal" process involves adding warm water to dissolve small, newly formed crystal nuclei (pseudocrystals) without melting the primary crystal seeds. This ensures that the final grains of monosodium glutamate vetsin are uniform in size and appearance.
Industrial-grade standards typically require a content of 99%, a PH range of 6.7-7.5, and very low levels of impurities, such as chloride at 0.1% and sulfate at 0.05%, to ensure safety and stability across various applications.
Conclusion
Monosodium glutamate vetsin stands as a cornerstone of modern flavor science, blending precise chemical engineering with practical culinary utility. From the rigorous control of crystallization and supersaturation to the strict adherence to purity standards (99% content and 98% transmittance), every step of its production is designed to ensure a high-quality, uniform product. Its versatility across the food, pharmaceutical, and laboratory sectors highlights its indispensable nature in enhancing the sensory and functional quality of diverse products.
As the industry moves toward more sustainable and automated manufacturing, the focus will likely shift toward further reducing the environmental footprint of the crystallization process and increasing the efficiency of mother liquor recovery. For businesses seeking a reliable supplier that balances technical precision with cost-effectiveness, choosing a manufacturer with a proven track record in quality control is paramount. Visit our website for more information: www.standard-seasoning.com