In the competitive landscape of global food additives, finding a reliable choline chloride manufacturer is essential for businesses seeking to enhance nutritional profiles and maintain strict quality standards. While often discussed in the context of livestock feed, the precision of chemical manufacturing allows these specialized providers to support a wide array of industrial food applications, ensuring that the end product meets international safety regulations.
The demand for high-purity additives has surged as consumers worldwide demand more transparent labeling and nutritionally fortified foods. A professional choline chloride manufacturer does not merely provide a raw ingredient but offers a critical link in the supply chain, ensuring that stabilizers and nutritional enhancers are delivered with consistent potency and purity across different batches.
Whether you are sourcing for pharmaceutical intermediates or advanced food seasoning, partnering with a certified choline chloride manufacturer ensures that your production line benefits from ISO-certified processes and global logistics expertise, reducing the risk of contamination and improving the shelf life of your final commercial products.
The Global Impact of a Choline Chloride Manufacturer
The operational scale of a modern choline chloride manufacturer extends far beyond local production, influencing food security and nutritional accessibility on a global scale. By optimizing the synthesis of essential additives, these manufacturers enable the creation of fortified foods that combat micronutrient deficiencies in developing regions, particularly across Africa and the Middle East.
Furthermore, the integration of ISO9001 and HACCP certifications within these factories ensures that the global movement of goods—via ocean, land, or air—meets the stringent sanitary requirements of importing nations. This systemic reliability allows food producers to scale their operations without fearing the volatility of raw material purity.
Defining the Role of a Choline Chloride Manufacturer
At its core, a choline chloride manufacturer is a specialized chemical entity focused on the production of a vital nutrient that serves as a precursor to acetylcholine and phospholipids. In the context of the food and feed additive industry, this role involves precise titration and stabilization to ensure the product remains effective under various storage conditions, such as high humidity or temperature fluctuations.
Beyond simple synthesis, the manufacturer acts as a quality guardian. They must bridge the gap between raw chemical engineering and food-grade safety, ensuring that no harmful residues remain in the product. This is particularly critical when the additives are destined for sensitive markets like the pharmaceutical or organic food sectors.
Ultimately, the manufacturer provides the fundamental building blocks that allow food scientists to create complex flavor profiles and nutritional supplements. Without the consistency provided by a professional choline chloride manufacturer, the scalability of mass-produced bouillon cubes or nutrient-enriched feed would be impossible.
Core Components of High-Quality Manufacturing
The first pillar of excellence for any choline chloride manufacturer is purity and consistency. Utilizing advanced filtration and crystallization techniques, the manufacturer ensures that each batch of the additive maintains a precise molecular weight and concentration, preventing variability in the final food product's taste or efficacy.
Scalability is another critical factor. A leading choline chloride manufacturer must possess the infrastructure to handle high-volume productivity, such as 500mt per month, while maintaining the agility to offer customized packaging options like 4g or 10g units to meet diverse client needs.
Finally, certification and compliance form the foundation of trust. By adhering to HALAL, FDA, and ISO22000 standards, a choline chloride manufacturer proves its commitment to safety and humanitarian needs, allowing its products to be seamlessly integrated into global markets without regulatory friction.
Global Applications and Industrial Use Cases
The applications of products from a choline chloride manufacturer are diverse, spanning from livestock nutrition to the enhancement of human food products. In the agricultural sector, these additives are essential for liver function and growth in poultry and swine, directly impacting the efficiency of global protein production.
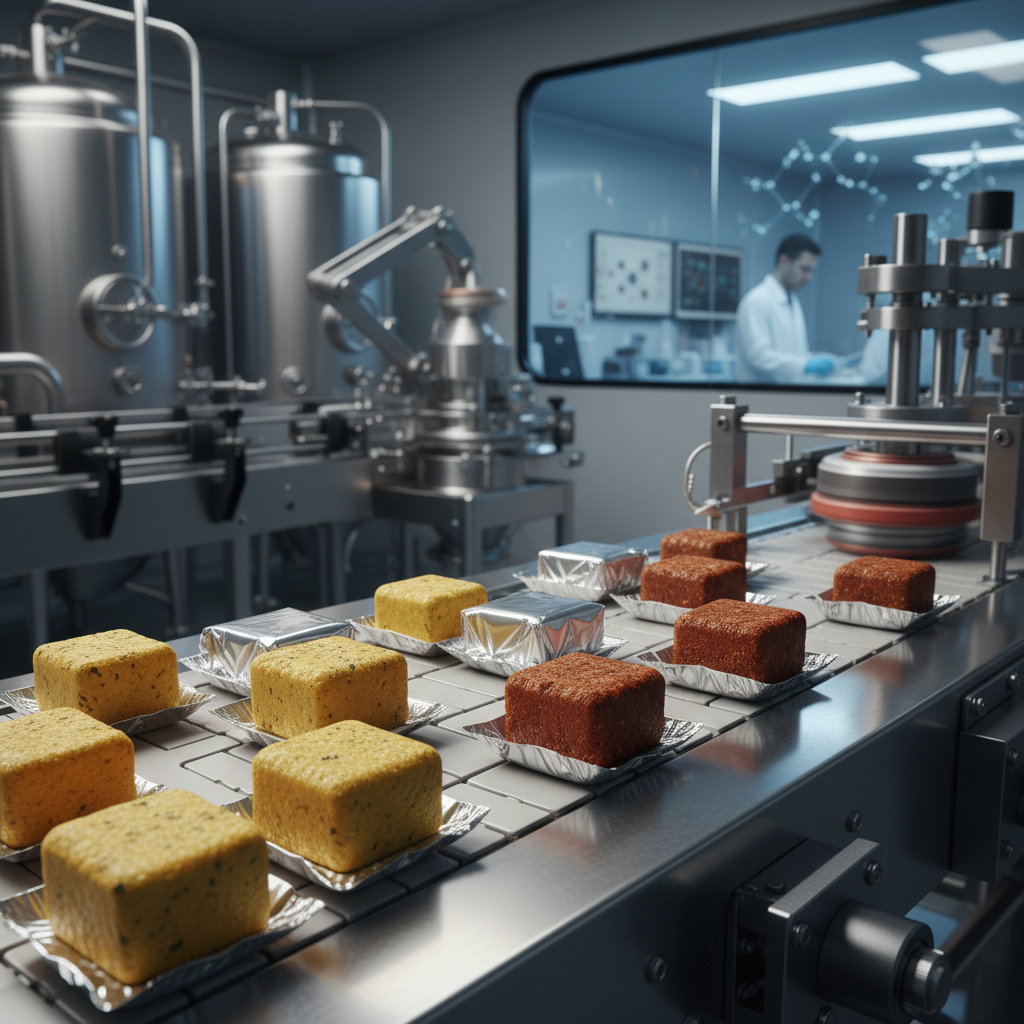
In the human food sector, the precision of a choline chloride manufacturer supports the production of savory seasonings and bouillon cubes. These products, often used in large-scale catering and home cooking across the Middle East and Africa, rely on high-quality additives to maintain flavor stability and nutritional value over a 24-month shelf life.
Efficiency Ratings by Choline Chloride Manufacturer Category
Long-Term Value and Strategic Advantages
Partnering with an established choline chloride manufacturer provides tangible economic advantages, primarily through the reduction of waste and the optimization of formulation costs. When the purity of an additive is guaranteed, food producers can use exact dosages, avoiding the over-utilization of ingredients and lowering the overall cost per unit.
Beyond the financial metrics, there is a significant emotional and logical value in reliability. Knowing that a supplier can consistently ship 1850 cartons per 20ft container within 7-15 days of deposit provides peace of mind to procurement managers, ensuring that production schedules are never interrupted by supply chain gaps.
Future Trends in Additive Production
The future of the choline chloride manufacturer lies in the transition toward "green chemistry." This involves reducing the carbon footprint of chemical synthesis and utilizing bio-based precursors to create additives that are not only effective but also sustainable, meeting the growing demand for eco-friendly food additives.
Digital transformation is also reshaping the industry. Leading manufacturers are implementing AI-driven quality control systems that can detect impurities at a molecular level in real-time, significantly reducing the margin of error and increasing the speed of batch approvals.
Furthermore, we are seeing a trend toward hyper-customization. The ability of a choline chloride manufacturer to provide tailored specifications—such as adjusting the solubility or granulation of the additive—allows food brands to create highly specialized products for niche dietary markets.
Challenges and Solutions in Supply Chain Management
One of the primary challenges faced by a choline chloride manufacturer is the volatility of raw material costs and the complexity of international logistics. Fluctuations in the price of chemical precursors can lead to pricing instability for the end consumer, requiring strategic hedging and long-term contracts.
To overcome these hurdles, many manufacturers are diversifying their transportation networks, offering a blend of ocean, land, and air freight to ensure that delivery timelines are met regardless of regional port congestion or geopolitical disruptions.
Another challenge is the strict divergence in regulatory requirements between different regions. A solution adopted by top-tier manufacturers is the implementation of a "Universal Compliance Framework," where products are manufactured to the highest possible global standard (e.g., combining FDA and EU standards), making the product viable for any market worldwide.
Analysis of Choline Chloride Manufacturer Operational Standards
| Metric Dimension |
Standard Process |
Advanced Process |
Impact Score (1-10) |
| Purity Testing |
Manual Batch Sampling |
Real-time HPLC Analysis |
9.5 |
| Packaging Speed |
Semi-Automatic Line |
Fully Robotic Filling |
8.0 |
| Logistics Reach |
Single Port Exit |
Multi-modal Hubs |
8.5 |
| Compliance |
Local Certification |
Global FDA/HALAL/ISO |
10.0 |
| Customization |
Standard Sizes Only |
Bespoke Packaging |
7.5 |
| Lead Time |
30+ Days |
7-15 Days |
9.0 |
FAQS
You should prioritize manufacturers who hold ISO9001, ISO22000, HACCP, and FDA certifications. For specific markets, HALAL and QS certifications are also critical to ensure the product is acceptable for regional consumption and meets stringent food safety and religious standards.
A professional manufacturer uses high-quality packaging materials, such as three-layer aluminum foil and five-layer corrugated cartons, which protect the additive from moisture and sunlight. This, combined with precise synthesis, ensures a shelf life of up to 24 months when stored in cool, dry conditions.
Yes, leading manufacturers offer customized packaging solutions. Common options include 4g or 10g cubes with various packing styles like side packing or envelope packing, allowing brands to tailor their product presentation to the specific preferences of their target consumers.
For a certified manufacturer with high productivity (e.g., 500mt/month), the typical shipping time is between 7 to 15 days upon receipt of the deposit. This efficiency is achieved through optimized production schedules and streamlined logistics at major ports like Qingdao.
Manufacturers maintain quality by using reinforced outer-packing (five-layer corrugated paper) and ensuring that loading patterns maximize stability in 20ft containers. This prevents physical damage and environmental contamination during the transit from China to markets in Africa or the Middle East.
Yes, manufacturers typically produce multiple grades including feed-grade, food-grade, and pharmaceutical-grade. Each grade has different purity requirements and testing protocols to ensure they are fit for their specific application, from livestock feed to human nutritional supplements.
Conclusion
In summary, the role of a professional choline chloride manufacturer extends far beyond the chemical synthesis of a single ingredient. By integrating rigorous quality certifications, scalable production capacities, and sophisticated logistics, these manufacturers provide the essential stability required for the global food and feed additive industries. From ensuring the nutritional integrity of bouillon cubes to supporting large-scale livestock operations, the impact of high-purity additive production is felt across the entire global food supply chain.
As the industry moves toward greener chemistry and AI-driven quality control, the strategic value of partnering with a transparent and certified manufacturer becomes even more critical. Businesses that prioritize purity, compliance, and supply chain reliability will be best positioned to meet the evolving demands of the global market. For those seeking a partner committed to these standards, we invite you to explore our solutions. Visit our website: www.chinaseasoning.com