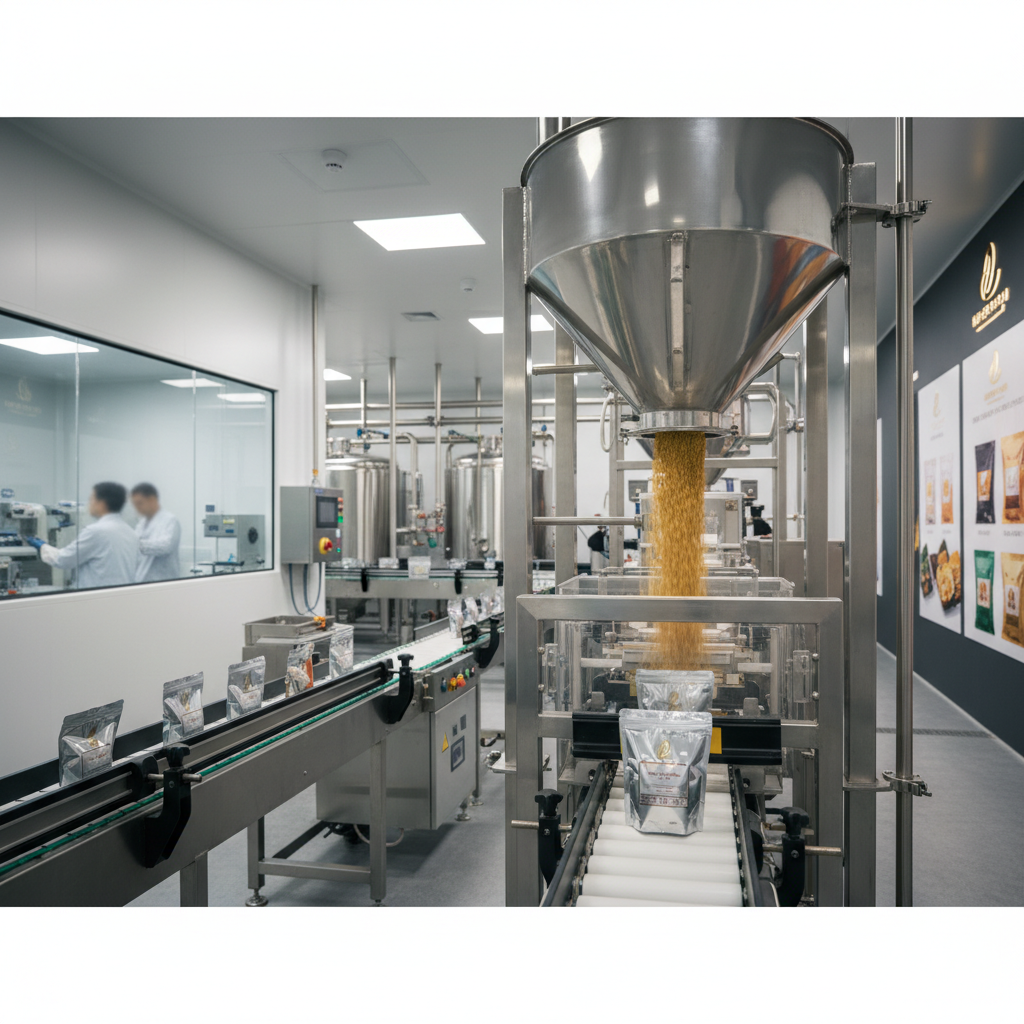
The modern food industry relies heavily on the precision and reliability of functional ingredients to ensure product stability and consumer satisfaction. Among the various components used, the role of a professional chemical additives in food supplier is critical in bridging the gap between raw natural extracts and high-performance industrial applications. By providing standardized additives, manufacturers can maintain consistent texture, shelf-life, and safety across global supply chains.
Sodium Alginate, a natural polysaccharide derived from brown algae, exemplifies the intersection of nature and chemistry. As a versatile hydrophilic colloid, it serves as a cornerstone for thickening and stabilizing in both food and pharmaceutical sectors. The ability to source this material from a reputable chemical additives in food supplier ensures that the molecular weight and viscosity parameters meet strict regulatory standards for food-grade consumption.
Whether used in the creation of bionic foods or as a stabilizer in beverages, the quality of the additive determines the final product's success. Finding a reliable chemical additives in food supplier allows brands to innovate with confidence, utilizing materials like Sodium Alginate to achieve precise gelation and viscosity control.
The Nature and Origin of Sodium Alginate
Sodium Alginate is a natural polysaccharide produced as a by-product of the extraction of iodine and mannitol from brown algae, specifically from kelp or Sargassum. Its molecular structure consists of β-D-mannuronic (M) and α-L-guluronic (G) acid units connected by (1→4) linkages. This unique biological makeup allows it to function as a high-stability excipient, making it a prized asset for any chemical additives in food supplier providing raw materials for pharmaceutical and food preparations.
Due to its inherent safety and solubility, Sodium Alginate is easily dissolved in water to form a viscous solution. This characteristic makes it an ideal hydrophilic colloid for various industrial uses, ranging from thickening agents in the food and beverage sector to specialized additives in printing pastes and oil formulations.
Technical Specifications and Quality Standards
For industrial procurement, the technical parameters of Sodium Alginate are the primary indicators of performance. A high-quality product typically maintains a viscosity range of 500-700 mPa.s and an 80-mesh fineness to ensure rapid dissolution and uniform distribution. Moisture levels are strictly controlled to a maximum of 15%, while the PH level remains balanced between 6.0 and 8.0 to maintain compatibility with other food ingredients.
Purity is non-negotiable when dealing with a chemical additives in food supplier. Heavy metal limits, such as Lead (Pb) at a maximum of 5.0 mg/kg and Arsenic (As) at a maximum of 2.0 mg/kg, are strictly monitored to meet global food safety standards. The appearance of the final product is typically a white or light yellow powder, signaling a clean extraction process.
Beyond the physical powder, the solubility is a key metric, with water-insoluble components kept below 0.6%. These rigorous specifications ensure that the Sodium Alginate behaves predictably during the manufacturing process, whether it is being used as a stabilizer in a beverage or as a thickening agent in a pharmaceutical gel.
The Chemistry of Gelation and Ion Exchange
One of the most fascinating properties of Sodium Alginate is its reaction to calcium ions. When alginate encounters calcium, a rapid ion exchange occurs, resulting in the formation of a thermally irreversible gel. This chemical reaction is the reason why a professional chemical additives in food supplier prioritizes the G/M ratio of the alginate they provide.
The structural integrity of the resulting gel depends on the proportion of guluronic acid (G) and mannuronic acid (M). High-G alginate produces gels that are hard but brittle, whereas high-M alginate results in flexible gels with lower hardness. By adjusting these ratios, a chemical additives in food supplier can provide materials tailored for specific textures, from firm bionic foods to soft, flexible masks.
This gelation capability extends beyond food. In environmental engineering, the gel properties are utilized for wastewater treatment agents, and in the packaging industry, they are used to create cling films. This versatility ensures that Sodium Alginate remains a high-demand product for global industrial distributors.
Practical Applications in Food and Industry
In the food industry, Sodium Alginate is primarily utilized as a thickener and stabilizer. Its ability to create stable emulsions and viscous textures makes it indispensable for sauces, dressings, and dairy alternatives. When sourced from a reputable chemical additives in food supplier, these materials ensure that the food maintains its structure during transport and storage.
Beyond simple thickening, the "spherification" technique in molecular gastronomy relies entirely on the ion-exchange gelation of alginate. By dropping a flavored liquid containing alginate into a calcium bath, chefs create bionic food pearls that burst with flavor. This innovative application demonstrates the transition of chemical additives from basic stabilizers to creative tools.
Sodium Alginate Performance Comparison by Grade
Strategic Advantages of Professional Sourcing
Partnering with a professional chemical additives in food supplier provides manufacturers with more than just raw materials; it provides supply chain security. With a productivity capacity of 500 MT per month, a reliable supplier can handle large-scale industrial demands while maintaining consistent quality across every 25kg bag produced.
Furthermore, the logistics expertise of a global supplier—offering ocean and land transportation from key ports like Qingdao—reduces lead times and operational costs. This allows companies to implement just-in-time inventory systems, reducing waste and ensuring that the Sodium Alginate used is always fresh and effective.
Sustainability and Environmental Impact
The extraction of Sodium Alginate is inherently sustainable, as it utilizes the biomass of brown algae. Many producers focus on the "waste liquid" from grass pulping processes, transforming what would be an environmental byproduct into a high-value industrial additive. This circular economy approach is a hallmark of a forward-thinking chemical additives in food supplier.
Moreover, because Sodium Alginate is a natural polysaccharide, it is biodegradable and non-toxic. This makes it a preferred alternative to synthetic polymers in applications like cling films and wastewater treatment agents, where reducing the carbon footprint and plastic pollution is a priority.
By leveraging natural marine resources, the industry reduces its reliance on petroleum-based chemicals. This shift not only meets regulatory requirements but also aligns with the growing consumer demand for "clean label" products in the food and pharmaceutical sectors.
Future Innovations in Food Additive Technology
The future of food additives lies in the precision tuning of molecular structures. We are seeing a trend toward "designer alginates," where the G/M ratio is precisely engineered to create specific textures for 3D food printing and advanced bionic materials. A leading chemical additives in food supplier is now integrating these precision techniques to serve the high-tech food science market.
Digital transformation in manufacturing is also playing a role. Automation in the extraction and purification process ensures that viscosity and purity remain constant regardless of the raw kelp source's seasonal variation. This level of consistency is vital for the pharmaceutical grade materials used in medical excipients.
As sustainability policies tighten, we expect to see more alginate-based alternatives to synthetic plastics and stabilizers. The evolution of Sodium Alginate from a simple thickener to a multi-functional bio-polymer represents the broader trajectory of the food additive industry toward safer, greener, and more efficient solutions.
Core Analysis of Sodium Alginate Industrial Applications
| Application Sector |
Primary Function |
Key Property Required |
Performance Score (1-10) |
| Beverage Industry |
Thickener/Stabilizer |
High Solubility |
9 |
| Pharmaceuticals |
Excipient/Gel Agent |
Ultra-High Purity |
10 |
| Molecular Gastronomy |
Spherification |
Rapid Gelation |
9 |
| Wastewater Treatment |
Flocculating Agent |
Ion Binding Capacity |
7 |
| Cosmetics (Masks) |
Film Forming |
Flexibility (High-M) |
8 |
| Oil Additives |
Viscosity Modifier |
Thermal Stability |
7 |
FAQS
The primary difference lies in the purity levels and the strictness of heavy metal controls. Food Grade Sodium Alginate, provided by a certified chemical additives in food supplier, must adhere to strict limits for Lead and Arsenic (e.g., Pb ≤ 5mg/kg) and possess a refined white or light yellow appearance. Industrial grade may have wider specifications for purity and are typically used in oil additives or wastewater treatment where human consumption is not a factor.
The ratio of guluronic (G) to mannuronic (M) acid determines the gel's physical properties. High-G alginates form strong, rigid, and brittle gels because the G-blocks bind more effectively with calcium ions. High-M alginates produce gels that are more flexible and softer. A professional chemical additives in food supplier can provide specific ratios based on whether you need a firm bionic food or a flexible medical dressing.
Yes, Sodium Alginate is an excellent natural alternative to synthetic polymers. Because it is a natural polysaccharide derived from brown algae, it helps brands achieve "clean label" status. It provides similar thickening and stabilizing properties without the chemical residues associated with some synthetic alternatives, provided it is sourced from a reliable chemical additives in food supplier.
Sodium Alginate is generally stable when stored in a cool, dry place away from direct sunlight. It is typically packaged in 25kg bags to prevent moisture absorption. While it has a long shelf life, it is important to ensure the packaging remains sealed to avoid clumps and maintain the moisture content below the 15% maximum specification.
No, the gel formed by the reaction of Sodium Alginate with calcium ions is thermally irreversible. This means once the gel is formed, it will not melt upon heating. This property is highly valued in the production of heat-stable food products and certain medical materials, distinguishing it from other gelling agents like gelatin.
Verification should involve reviewing the Certificate of Analysis (CoA) for each batch, checking for ISO or Food Grade certifications, and verifying parameters such as viscosity (500-700 mPa.s), mesh size (80 mesh), and heavy metal content. A transparent supplier will provide these specifications and samples for testing before large-scale procurement.
Conclusion
Sodium Alginate stands as a testament to the power of natural chemistry in modern industry. From its origin in brown algae to its application in high-end molecular gastronomy and critical pharmaceutical excipients, its versatility is unmatched. The ability to control texture through G/M ratios and ion exchange allows for endless innovation in product development, provided the raw materials are sourced from a precise and high-capacity chemical additives in food supplier.
As the global market shifts toward sustainable and bio-based ingredients, the importance of high-purity, naturally derived additives will only grow. Manufacturers are encouraged to prioritize suppliers who offer both technical transparency and scalable production to ensure long-term stability and safety. To explore premium food-grade solutions and secure your supply chain, visit our website: www.standard-seasoning.com.