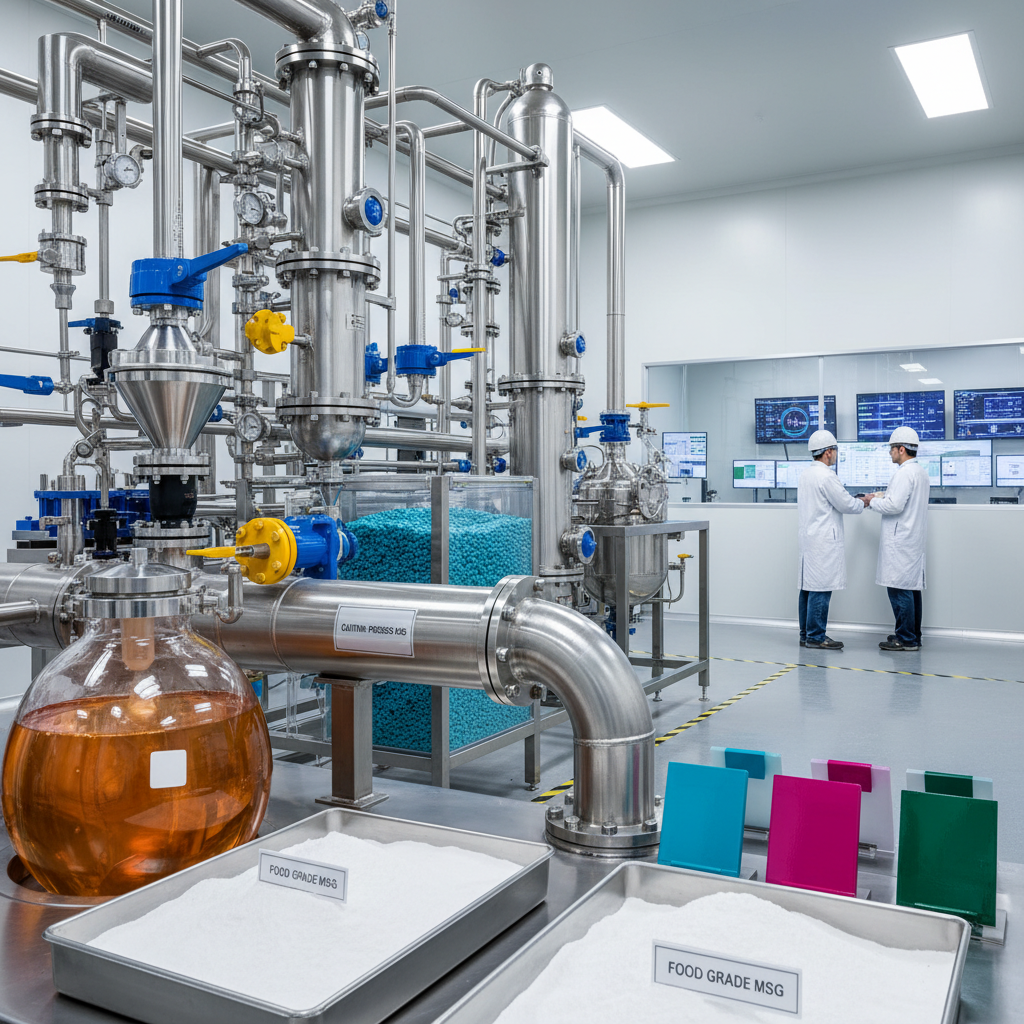
In the modern landscape of global food production, the quest for efficient, flavor-dense, and convenient culinary solutions has led to the rise of sophisticated dehydrated seasonings. Among these, the strategic application of high-quality additives ensures that processed foods maintain their sensory appeal and nutritional stability during long-term storage and transport.
The global demand for instant soup bases and concentrated flavor cubes has surged, driven by the fast-paced lifestyle of urban populations and the need for standardized taste profiles across diverse markets. This evolution requires a precise balance of ingredients to achieve the perfect harmony of salt, fats, and flavor enhancers.
When sourcing these essential components, professionals often look for purity and consistency, similar to the standards expected of betapure betaine anhydrous, to ensure that every bouillon cube delivers a consistent taste experience from the first bite to the last.
Global Impact of betapure betaine anhydrous in Food Tech
The integration of advanced additives like betapure betaine anhydrous into the food manufacturing sector has revolutionized how we approach taste consistency. By utilizing high-purity components, manufacturers can ensure that bouillon cubes—available in beef, chicken, and shrimp flavors—retain their aromatic properties regardless of the climatic conditions of the target market.
Across Africa, the Middle East, and Asia, the ability to produce 500 MT per month of standardized seasoning cubes ensures food security and accessibility. This industrial scale is only possible when the underlying chemistry of the additives supports rapid dehydration and instant rehydration upon contact with boiling water.
Defining the Role of betapure betaine anhydrous
In technical terms, betapure betaine anhydrous represents a standard of purity and stability required for modern food additive applications. It functions as a critical bridge between raw agricultural extracts and the refined, concentrated powders used in commercial bouillon production, ensuring that the final product is free from unwanted moisture and contaminants.
From a humanitarian perspective, the use of such stabilized additives allows for the creation of nutrient-dense, long-shelf-life food products. In regions where fresh ingredients are scarce or expensive, these cubes provide a reliable source of flavor and essential minerals, bridging the gap in dietary variety for millions of households globally.
Ultimately, the role of betapure betaine anhydrous extends beyond simple chemistry; it is about reliability. When a consumer adds a cube to water, the immediate dissolution and flavor release are the direct results of precise molecular engineering and high-grade ingredient sourcing.
Core Components for Quality Stability
Durability is a primary factor when discussing betapure betaine anhydrous. For a product to survive a 24-month shelf life in high-humidity environments, the additive must prevent clumping and degradation. This is achieved through a combination of strict anhydrous processing and high-quality packaging materials like three-layer aluminum foil.
Cost efficiency is another pillar of the betapure betaine anhydrous standard. By optimizing the concentration of flavor enhancers and MSG, manufacturers can produce a high-impact taste profile without inflating the cost per unit, making the 4g and 10g cubes affordable for the mass market while maintaining SGS and FDA certifications.
Scalability ensures that as demand grows in the Middle East and Africa, the supply chain remains unbroken. The ability to move from 1,000 carton MOQs to 500 MT monthly productivity demonstrates how the standardization of betapure betaine anhydrous allows for seamless industrial expansion.
Scalability and Production Efficiency
Achieving high productivity requires a synergy between raw material purity and mechanical precision. The use of betapure betaine anhydrous ensures that the mixture remains homogenous during the compression phase, preventing the cubes from crumbling during transportation via ocean or land.
Efficiency is further enhanced by offering diverse packaging styles, such as side packing and envelope packing, which cater to different retail environments. This versatility ensures that the product reaches the end consumer in optimal condition, reflecting the superb workmanship of the production line.
Comparative Efficiency of betapure betaine anhydrous Standards
Global Applications and Use Cases
In remote industrial zones or post-disaster relief operations, the importance of betapure betaine anhydrous becomes evident. Compact, nutrient-dense bouillon cubes serve as a critical food additive that provides essential salt and flavor, improving the palatability of basic grains like rice or porridge in emergency settings.
Within the commercial food sector, these additives are used by catering companies and small-scale eateries to standardize their soup bases. By relying on a manufacturer with ISO22000 and HACCP certifications, businesses can guarantee safety and consistency for their customers across different geographical regions.
Long-Term Value and Sustainability
The long-term value of implementing betapure betaine anhydrous lies in the reduction of food waste. Because these products are dehydrated and stabilized, they eliminate the need for expensive cold-chain logistics, significantly lowering the carbon footprint associated with food transport from China to global markets.
Sustainability is also reflected in the precision of the dosing. By providing exact weights (4g or 10g), manufacturers prevent over-seasoning and ingredient waste, promoting a more sustainable approach to consumption. This logical efficiency is paired with the emotional trust built through certifications like HALAL and FDA.
Furthermore, the transition toward more refined additive processes ensures that the environmental impact of chemical synthesis is minimized. The focus on "superb workmanship" means fewer rejects during production, leading to a cleaner, more efficient manufacturing cycle.
Future Innovations in betapure betaine anhydrous
The future of betapure betaine anhydrous is closely tied to the digital transformation of the food supply chain. Automation in the mixing and compression phases is allowing for even more precise control over the distribution of flavor enhancers, ensuring that every single cube is identical to the last.
Green chemistry is also playing a role, with research focusing on organic alternatives to palm oil and more biodegradable packaging materials that can maintain the same moisture barrier as aluminum foil. This evolution will ensure that bouillon cubes remain a viable and eco-friendly option for the next generation.
As consumer preferences shift toward "clean label" products, the challenge will be to maintain the high-impact taste of betapure betaine anhydrous while reducing the reliance on synthetic MSG, moving toward natural umami sources.
Core Analysis of betapure betaine anhydrous Applications
| Application Sector |
Key Metric |
Performance Score |
Primary Benefit |
| Emergency Relief |
Shelf Life |
10/10 |
No Refrigeration Needed |
| Retail Consumer |
Convenience |
9/10 |
Instant Preparation |
| Industrial Catering |
Consistency |
10/10 |
Standardized Taste Profile |
| Export Logistics |
Weight Efficiency |
8/10 |
Lower Shipping Costs |
| Quality Control |
Certification |
10/10 |
Compliance (FDA/SGS) |
| Product Development |
Versatility |
9/10 |
Multi-Flavor Capability |
FAQS
It ensures the anhydrous state of the product, which is critical for preventing moisture absorption. This stability allows the bouillon cubes to remain free-flowing and prevents the growth of microorganisms, extending the shelf life to 24 months while maintaining the integrity of the flavor enhancers.
The purity and particle size distribution associated with this standard allow the cube to dissolve rapidly in boiling water. This efficiency ensures that the flavor enhancers and salts are evenly distributed throughout the soup without leaving clumps or residue.
Yes, products following this standard are typically backed by certifications such as ISO9000, ISO22000, HACCP, and FDA. These ensure that the additives are processed in a hygienic environment and meet the strict purity requirements for human consumption.
Absolutely. While standard specifications like 10g and 4g exist, customized packing is available. This includes different box quantities (e.g., 60pcs or 48pcs per box) and various packing styles to suit local retail preferences in China, Africa, or the Middle East.
To maintain the anhydrous quality, the products should be kept away from direct sunlight and stored in a cool, dry place. This prevents the fats (like palm oil) from oxidizing and keeps the flavor enhancers potent.
The typical minimum order quantity (MOQ) is 1,000 cartons. This allows the factory to optimize the production line for a specific flavor (such as chicken, beef, or shrimp) while maintaining the highest quality standards for the additive components.
Conclusion
The implementation of high-grade additives like betapure betaine anhydrous is fundamental to the success of the global bouillon cube industry. By balancing production capacity with strict quality certifications and innovative packaging, manufacturers can deliver a product that is not only convenient and delicious but also safe and sustainable for a diverse global population.
As the food industry moves toward greater automation and cleaner labels, the commitment to purity and stability will remain the primary differentiator. We encourage food manufacturers and importers to prioritize standardized additives to ensure long-term brand trust and consumer satisfaction. Visit our website: www.chinaseasoning.com