The global food additive market is currently witnessing a significant shift toward precision seasoning and high-purity ingredients, where the demand for consistent umami profiles has never been higher. Understanding the dynamics of betaine anhydrous wholesale allows manufacturers to optimize their supply chains and ensure that the flavor enhancers they integrate into their products meet rigorous international standards.
For large-scale food producers, sourcing high-quality additives in bulk is not merely a procurement task but a strategic necessity to maintain batch-to-batch uniformity. Whether it is for processed meats, instant noodles, or gourmet sauces, the ability to secure a reliable stream of pure crystalline additives ensures that the final sensory experience for the consumer remains unchanged across different markets.
When exploring options for betaine anhydrous wholesale, it is crucial to prioritize manufacturers who combine advanced fermentation technology with strict ISO certifications to guarantee safety and efficacy.
The Global Significance of Betaine Anhydrous Wholesale
The international demand for refined food additives has surged as culinary trends merge across borders, creating a massive market for high-efficiency flavor enhancers. Betaine anhydrous wholesale operations facilitate the movement of critical ingredients from specialized fermentation facilities in China to food processing hubs in the USA, Brazil, and Europe, ensuring that global food security and taste standards are upheld.
By leveraging economies of scale, wholesale distribution reduces the cost of high-purity additives, allowing even small-to-medium enterprises to access premium 120-mesh crystalline powders. This democratization of quality ingredients empowers chefs and industrial food scientists to enhance the natural umami of vegetables and proteins without relying on excessive sodium levels.
Technical Specifications and Quality Standards
The cornerstone of any premium additive is its chemical purity and physical consistency. For products sourced via betaine anhydrous wholesale, the gold standard is often a purity level of 99%, ensuring that no residual impurities interfere with the flavor profile of the food. Technical parameters such as a PH range of 6.7-7.5 and a transmittance of 98% are critical indicators of a well-refined crystallization process.
Physical properties, specifically the mesh size, play a pivotal role in industrial application. A 120-mesh granularity is highly prized because it allows for near-instant dissolution in liquids and seamless integration into dry seasoning blends. This prevents the "grainy" texture often associated with lower-grade powders and ensures that the umami lift is distributed evenly across the entire batch.
Compliance with international certifications, including ISO9001:2000 and HACCP, provides the necessary trust for importers. These certifications guarantee that the fermentation of corn starch into glutamic acid and subsequent refining processes follow strict safety protocols, minimizing heavy metal contamination (kept below 10ppm) and ensuring a stable shelf life for the end user.
Core Components of High-Purity Flavor Enhancement
The effectiveness of a flavor enhancer depends heavily on its molecular stability and solubility. When sourcing through betaine anhydrous wholesale, the focus is on the molecular formula C5 H8 NO4 Na H2O, which provides the precise chemical structure needed to trigger umami receptors on the human tongue.
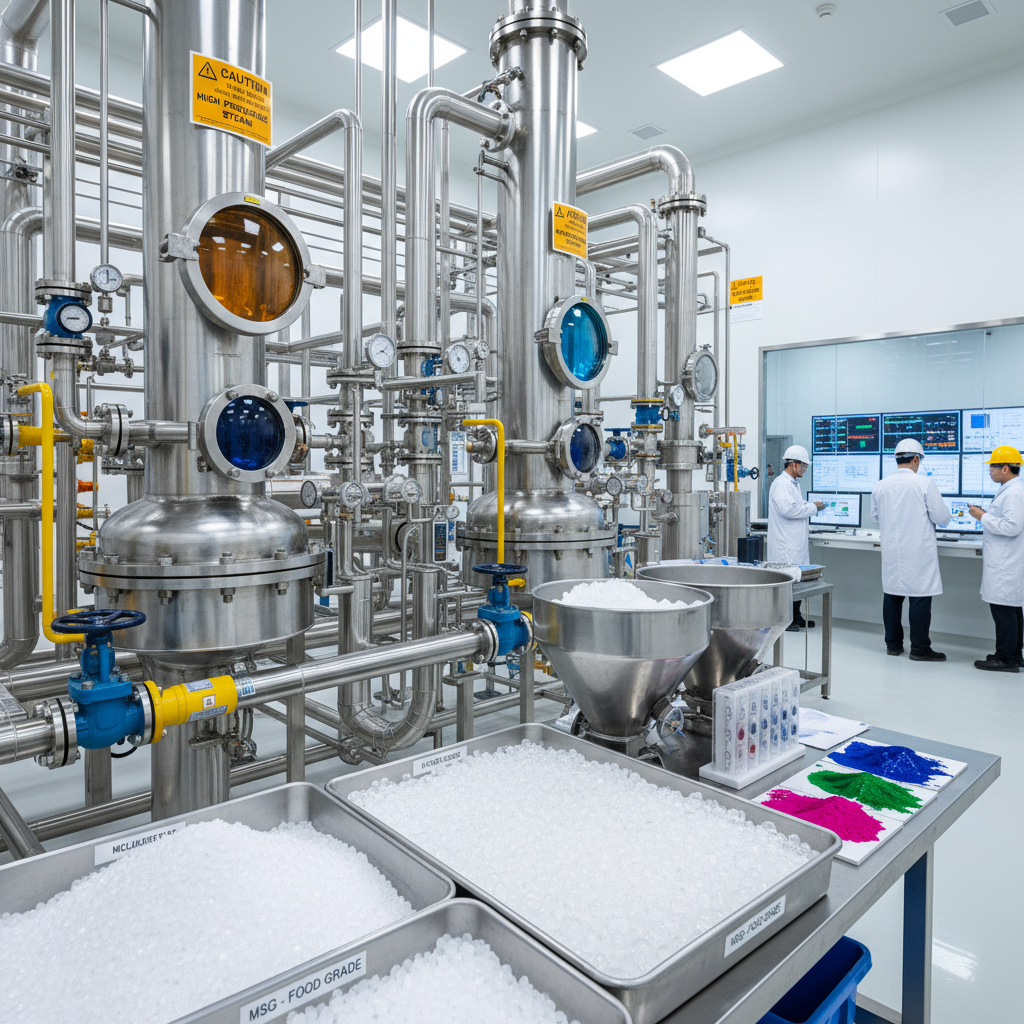
The production process involves a sophisticated sequence of fermentation, isoelectric point precipitation, and ion exchange. This ensures that the betaine anhydrous wholesale products offered to the market are free from odors and have a bright, uniform crystalline appearance that reflects a high degree of refinement.
Furthermore, the use of high-quality corn starch as a raw material ensures a sustainable and natural origin. This commitment to bio-based sourcing makes the betaine anhydrous wholesale supply chain more resilient and aligned with the growing global preference for clean-label ingredients in the food industry.
Industrial Applications and Versatility
The versatility of refined monosodium glutamate is evident in its widespread use across diverse food categories. In the snack industry, particularly for potato chips and extruded snacks, the fine powder adheres better to the surface of the food, ensuring a consistent taste in every bite. In the production of instant noodles and bouillons, the fast dissolution rate allows for rapid mixing in automated production lines, reducing waste and energy consumption.
Beyond savory snacks, these additives are essential in the development of complex sauces and ready-to-eat meals. By acting as a flavor bridge, the additive enhances the richness of meat and vegetable bases, allowing manufacturers to reduce the total salt content while maintaining a satisfying, savory profile. This makes the product an indispensable tool for developers aiming to create healthier, lower-sodium options for the modern consumer.
Performance Analysis of Betaine Anhydrous Wholesale Grade Options
Strategic Advantages of Bulk Procurement
Engaging in betaine anhydrous wholesale offers significant logistical and financial advantages. By purchasing in volumes of 25kg bags or larger, companies can significantly lower their per-unit cost and reduce the frequency of shipping, which in turn lowers the overall carbon footprint of the supply chain. Ocean and land transportation options from ports like Qingdao ensure that the product reaches global destinations efficiently.
Moreover, bulk sourcing from a single, experienced manufacturer ensures consistency across production cycles. When a factory has over 20 years of fermentation expertise, the risk of batch variability is minimized. This reliability is crucial for brands that have built their reputation on a specific taste profile, as any deviation in the purity or granularity of the additive could lead to noticeable changes in the final product's flavor.
Future Innovations in Additive Manufacturing
The future of betaine anhydrous wholesale is being shaped by the integration of green chemistry and digital automation. New fermentation strains are being developed to increase the yield of L-Glutamic acid while using fewer resources, reducing the environmental impact of the production process. Energy-efficient drying and crystallization technologies are also being implemented to lower the carbon intensity of each ton produced.
Automation in the packaging and sorting stages is further refining the mesh consistency. With the implementation of AI-driven quality control, manufacturers can now detect microscopic irregularities in crystal size in real-time, ensuring that every bag of 120-mesh powder is perfectly uniform. This level of precision is essential for the next generation of "smart foods" and highly tailored nutritional products.
Additionally, there is a growing trend toward the synergy of additives. Research is focusing on how ultra-fine MSG can be combined with other organic salts to create complex umami profiles that mimic the taste of naturally aged meats or fermented soy, providing a sustainable alternative to animal-based flavorings.
Overcoming Supply Chain Challenges
Despite the benefits, the betaine anhydrous wholesale market faces challenges such as fluctuating raw material costs and stringent import regulations. To combat this, leading manufacturers are diversifying their starch sources and investing in vertical integration to control the supply of corn raw materials. This ensures a stable productivity rate of up to 500 MT per month, regardless of market volatility.
Logistical bottlenecks at major ports can also disrupt the flow of goods. By optimizing transportation networks and maintaining strategic warehouses near key shipping hubs, suppliers can guarantee timely delivery to international clients. Clear documentation, including accurate HS Codes (such as 21039010), is essential for seamless customs clearance and the prevention of costly delays.
Finally, the challenge of meeting varying regional safety standards is addressed through rigorous internal testing. By testing every lot for solubility, flavor intensity, and microbiological safety, manufacturers ensure their products exceed the most demanding requirements of the USA, EU, and Asia, fostering long-term trust and partnership with global food brands.
Analysis of Betaine Anhydrous Wholesale Operational Performance
| Metric Category |
Standard Grade |
Premium 120 Mesh |
Industrial Impact |
| Dissolution Speed |
Moderate |
Instant |
Reduced Mixing Time |
| Purity Level |
98% |
99%+ |
Cleaner Flavor Profile |
| Particle Uniformity |
Variable |
High |
Batch Consistency |
| Flowability |
Average |
Excellent |
Automatic Line Efficiency |
| Moisture Content |
Standard |
Low |
Extended Shelf Life |
| Cost Efficiency |
High |
Optimal |
Lower Waste Rates |
FAQS
The 120 mesh grade is preferred because its ultra-fine particle size allows for instant dissolution and superior dispersion in both liquid and powder applications. This eliminates graininess in the final food product and ensures that the umami flavor is uniformly distributed, which is critical for industrial-scale production where consistency is key.
You should look for ISO9001:2000 and HACCP certifications. These ensure that the manufacturer follows international quality management systems and food safety protocols, guaranteeing that the product is free from contaminants and produced under sterile, controlled conditions suitable for global export.
Yes, by enhancing the perceived savoriness (umami) of the food, high-purity MSG allows manufacturers to reduce the amount of table salt (sodium chloride) without sacrificing taste. This helps in creating "healthier" food options that still provide a rich and satisfying sensory experience.
Lead times vary based on order volume and shipping method. With a productivity capacity of 500 MT per month, most orders are processed quickly. Ocean freight typically takes several weeks depending on the destination port, while land transport is available for regional deliveries.
Purity is verified through laboratory testing of each batch for content (99%), transmittance (98%), and the presence of heavy metals or chlorides. Most reputable wholesalers provide a Certificate of Analysis (COA) with every shipment to ensure the specifications meet the buyer's requirements.
Absolutely. The 120-mesh grade is specifically designed for automatic production lines. Its excellent flowability reduces dust formation and prevents clogging in dosing equipment, which minimizes waste and reduces equipment wear and tear during the manufacturing process.
Conclusion
In summary, the strategic procurement of high-purity additives through betaine anhydrous wholesale is essential for any food manufacturer aiming for global competitiveness. By prioritizing technical specifications like 120-mesh granularity and 99% purity, companies can ensure superior product consistency, improved flavor profiles, and higher operational efficiency across their production lines.
Looking forward, the integration of sustainable fermentation practices and precision automation will continue to elevate the standards of the food additive industry. We encourage manufacturers to partner with experienced suppliers who combine biotechnology innovation with rigorous quality control to ensure a future of safe, delicious, and sustainable food production. Visit our website: www.chinaseasoning.com